Explore our elite portfolio of high-purity, client-focused plant extracts and functional powders designed for diverse regulatory and application needs.
Flavonoids represent a critical class of secondary metabolites widely distributed in the plant kingdom, appreciated globally for their anti-inflammatory, antioxidant, cardio-protective, and anti-aging properties. As target biological systems become more complex and consumer markets demand higher efficacy, the development of functional food, health supplements, and daily cosmetics hinges on sourcing highly bioavailable and chemically stable flavonoids.
Through our dedicated ODM Flavonoid Solutions, we address key formulation hurdles like chemical oxidation, poor solubility, and variable absorption profiles. Botanical Cube Inc. acts not merely as a raw materials supplier but as an integrated development partner. We offer specialized scientific backing to optimize chemical structure preservation, enabling you to build superior consumer products that drive shelf success and commercial trust.
By using custom extraction pathways, including supercritical fluid systems and membrane separation, we guarantee a standardized concentration of active flavonoids. This minimizes inert biomass residues while maximizing molecular potency.
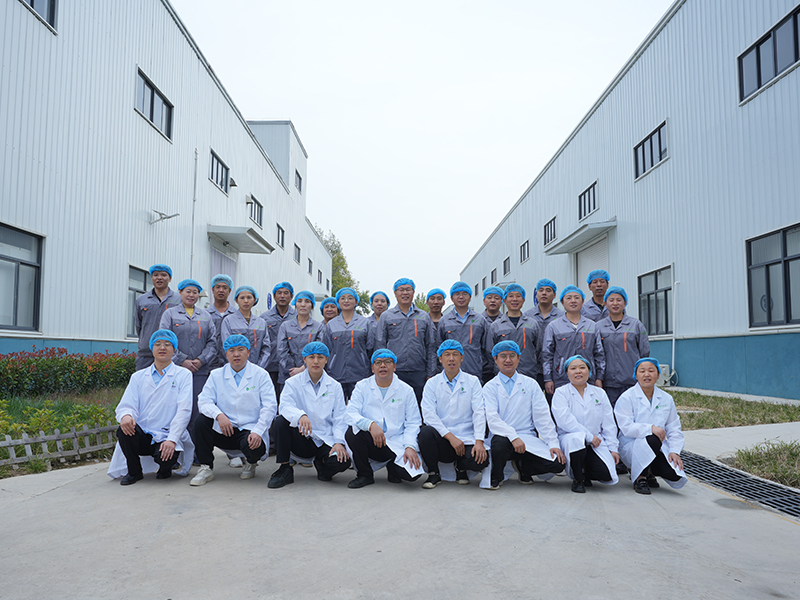
Deep industry experience powered by strong parent infrastructure and state-of-the-art processing bases.
Benefiting from the solid foundation provided by its parent company, Xi'an Tianben Bioengineering Co., Ltd., Botanical Cube Inc. focuses on researching, developing, producing, and selling healthy natural ingredients. With more than two decades of industry experience, it has become a leader in the field, specializing in providing high-quality plant extracts and customized solutions to global customers. Our services meet the needs of industries including herbal medicine, health foods, dietary supplements, food and beverages, daily chemicals, and cosmetics.
Our operations are supported by three companies — Xi'an Tianben Bioengineering Co., Ltd., Botanical Cube Inc., and Shaanxi Tianben Kangyuan Biotechnology Co., Ltd. — which together operate 3 production bases covering more than 100 acres and process more than 3,000 tons of plant raw materials each year. The product range includes more than 200 plant extracts, and we also provide a variety of certified organic products to meet the global demand for environmentally friendly and healthy solutions. Exporting to 60% of the world's countries, we serve more than 200 countries and regions and over 500 customers from all walks of life.
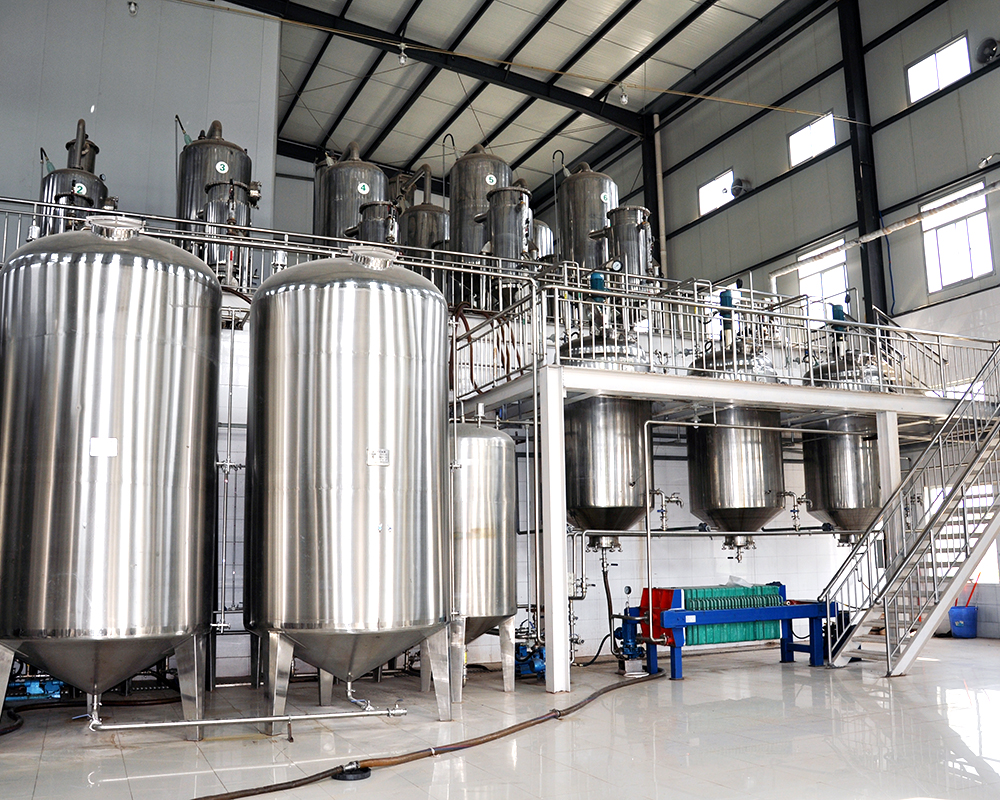
Our first factory was established in 2012 in Sanyuan City, Xi'an, four years after our company was founded. At that time, our production experience was still in its early stages, and we faced many challenges as we worked to refine our processes. However, we remained committed to continuous improvement, investing heavily in technology, training, and quality control to strengthen our capabilities. These early efforts laid a strong foundation for our future growth, shaping the high standards of excellence that we uphold today.
Now, our facility utilizes modern automation and sterile engineering designs to keep batch-to-batch variation at an absolute minimum, ensuring that chemical profiles meet standard HPLC reference points perfectly.
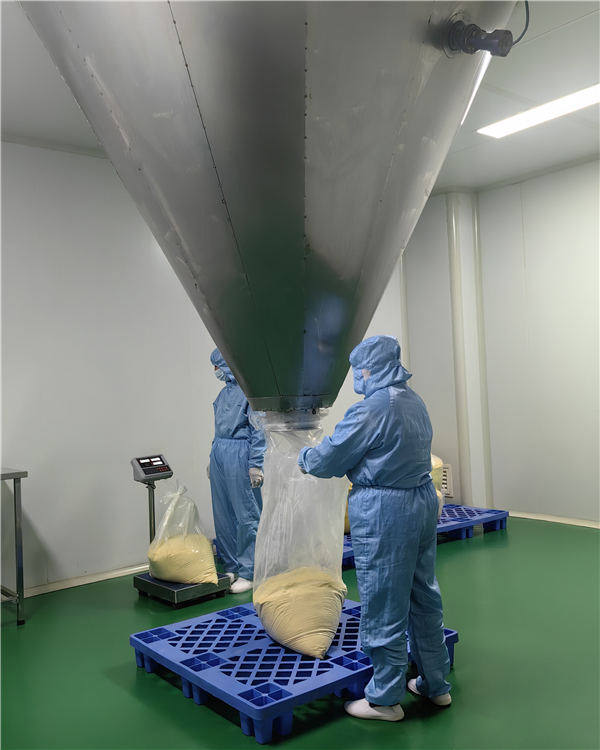
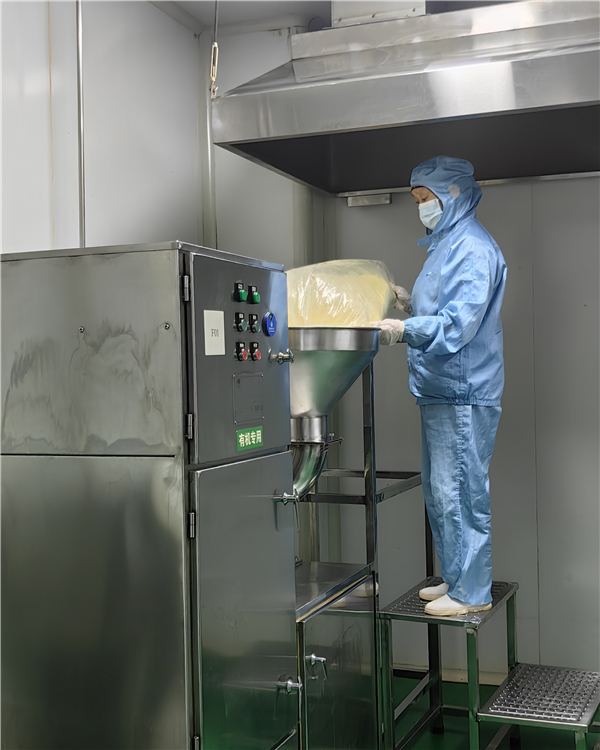
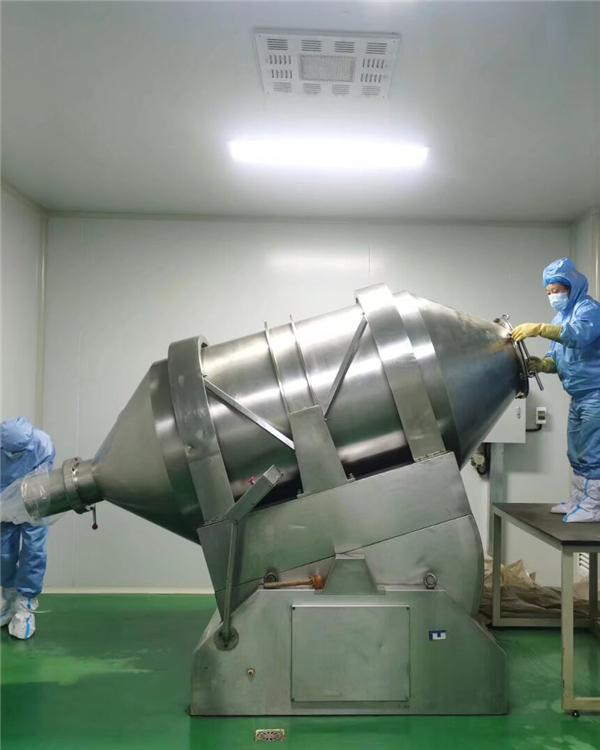
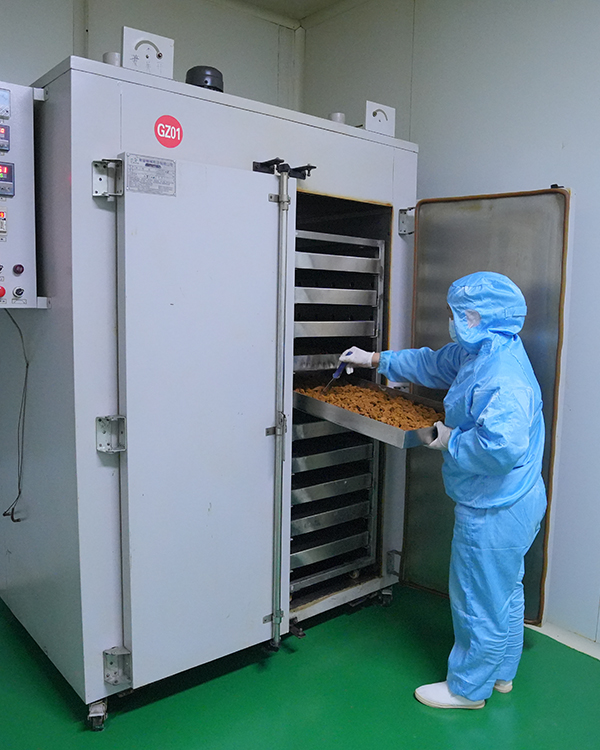
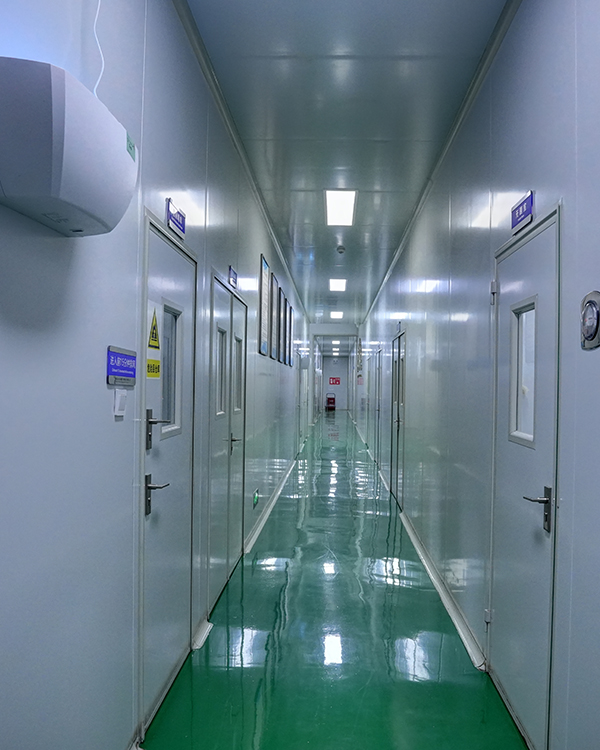
Powder collection, crushing and sieving, mixing, and drying processes are all performed in a Class 100,000 cleanroom environment. Our operators strictly follow hygiene protocols and wear sterile gowns, masks, and gloves to maintain product purity and safety, thus ensuring that we provide our customers with high quality standards and reliable ingredients.
Pioneering molecular stability, structural integrity, and nano-carriers for bio-enhancement.
Natural flavonoids suffer from poor water solubility. Our R&D team works to encase active molecules in protective lipid shells. This enhances bioavailability and supports sustained release inside the gut, ensuring functional benefits last longer.
By utilizing targeted bio-enzymatic glycosylation, we alter the solubility profile of specific flavones and catechins. This prevents precipitations in neutral beverages, making them ideal for the functional ready-to-drink (RTD) market.
We are transitioning to supercritical water extraction and subcritical ethanol systems. These methods minimize chemical waste, reduce the carbon footprint, and prevent solvent residue contamination in our organic product range.
Providing customized formulation matrices, regulatory support, and batch scaling across vertical markets.
We supply heat-stable, clear, taste-masked flavonoids designed for energy bars, sports nutrition powders, and antioxidant drinks. Our formulations remain stable through pasteurization and long-term shelf storage.
We offer high-density powders and direct-compressible granules optimized for encapsulation and tableting. Our team works to prevent dynamic crystallization, which helps avoid crumbling or capping during high-speed production.
Our cosmetic-grade flavonoids, such as catechins and gallic acid derivatives, offer clinically proven benefits. They serve as potent anti-aging, UV-protective, and skin-brightening agents that blend smoothly into topical emulsions.
We produce ultra-purified flavonoid APIs under strict cleanroom conditions. These meet international pharmacopoeia standards, with full HPLC validation and comprehensive documentation for clinical evaluations.
Operating out of Shaanxi, China, our manufacturing facilities integrate modern agricultural supply lines with advanced processing automation. By positioning ourselves near primary cultivation zones, we ensure direct sourcing control, which reduces transport-related deterioration of raw botanical compounds.
Our intelligent storage systems continuously monitor humidity and temperature, protecting raw botanicals before extraction. This reliable setup helps protect our partners from fluctuating market supply, crop failures, or global shipping bottlenecks.
Additionally, our digital traceability program tracks every batch from the initial field harvest through to the final packaged powder. This complete transparency is essential for modern compliance reviews.
Providing clear documentation, localized regulatory support, and independent quality testing for overseas markets.
Our facilities operate in strict compliance with ISO, GMP, Kosher, Halal, and organic certifications. This simplifies your regulatory reviews and speeds up product launches.
Every batch of powder undergoes rigorous testing via ICP-MS and GC-MS. This guarantees that impurities remain well below the limits set by FDA, EFSA, and USP regulations.
We work with local logistics centers in North America and Europe to offer flexible cargo options, minimizing custom delays and reducing shipping times for critical orders.
Essential insights for procurement managers, R&D teams, and quality assurance specialists.
Providing diverse bio-nutrients, functional plant extracts, and active powders to support global wellness brands.
 Botanical