The global health supplements industry is undergoing a profound structural evolution, shifting rapidly from synthetic compounds to clinically-backed botanical extracts and natural nutraceuticals. Within the South Pacific, the Kingdom of Tonga represents a unique micro-market characterized by an increasing demand for preventive healthcare solutions, addressing lifestyle-related metabolic concerns, and elevating community wellness standards through imported high-purity biological ingredients.
Sourced from certified clean-room facilities, meeting stringent international quality verification standards.
Benefiting from the solid foundation provided by its parent company, Xi'an Tianben Bioengineering Co., Ltd., Botanical Cube Inc. focuses on researching, developing, producing and selling healthy natural ingredients. With more than two decades of industry experience, it has become a leader in the field, specializing in providing high-quality plant extracts and customized solutions to global customers. Services meet the needs of industries including herbal medicine, health foods, dietary supplements, food and beverages, daily chemicals and cosmetics.
Our operations are supported by three companies - Xi'an Tianben Bioengineering Co., Ltd., Botanical Cube Inc. and Shaanxi Tianben Kangyuan Biotechnology Co., Ltd. - which together operate 3 production bases covering more than 100 acres and process more than 3,000 tons of plant raw materials each year. The product range includes more than 200 plant extracts, and we also provide a variety of certified organic products to meet the global demand for environmentally friendly and healthy solutions. Exporting to 60% of the world's countries, serving more than 200 countries and regions and more than 500 customers from all walks of life.
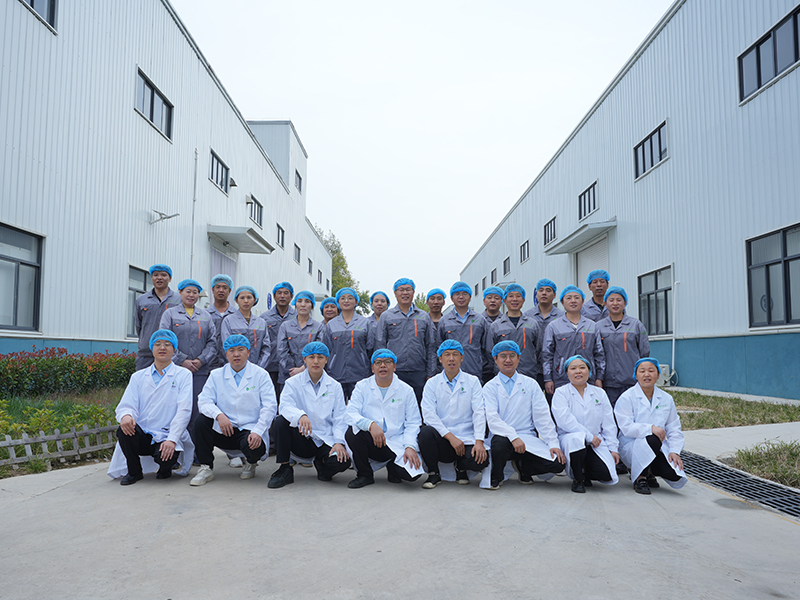
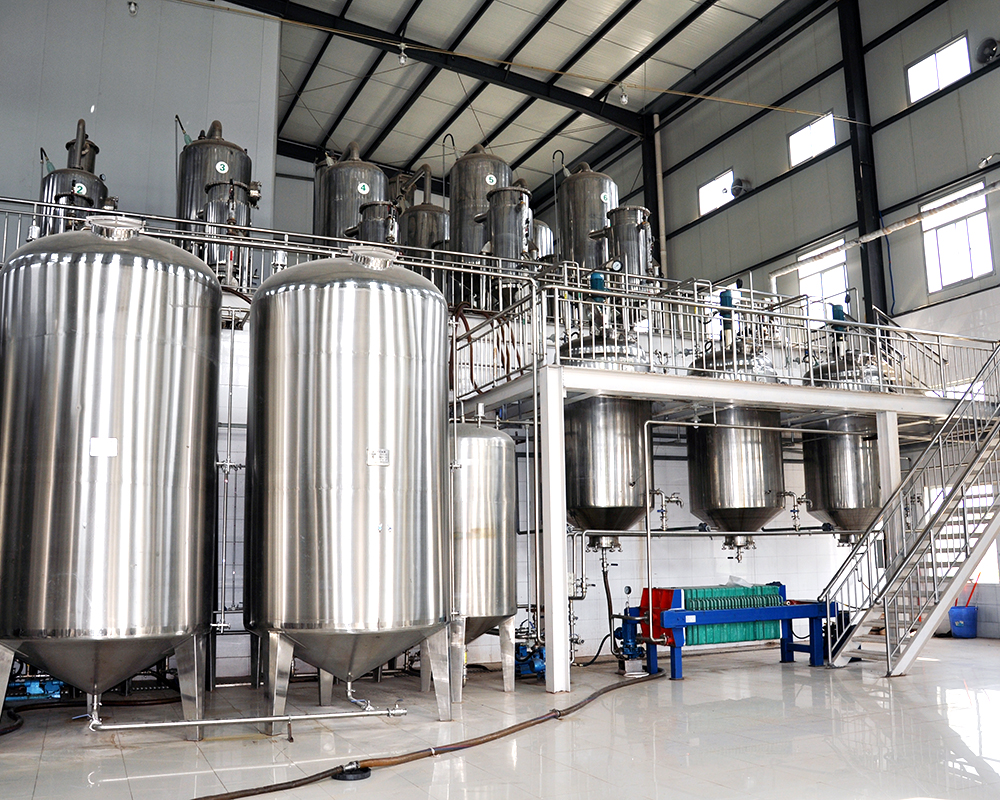
Our first factory was established in 2012 in Sanyuan City, Xi'an, four years after our company was founded. At that time, our production experience was still in its early stages, and we faced many challenges as we worked to refine our processes. However, we remained committed to continuous improvement, investing heavily in technology, training, and quality control to strengthen our capabilities. These early efforts laid a strong foundation for our future growth, shaping the high standards of excellence that we uphold today.
Powder collection, crushing and sieving, mixing and drying processes are all performed in a Class 100,000 cleanroom environment. Our operators strictly follow hygiene protocols and wear sterile gowns, masks and gloves to maintain product purity and safety, thus ensuring that we provide our customers with high quality standards and reliable ingredients.
As consumer expectations shift toward personalized nutrition and certified organic efficacy, the dietary supplements sector is deploying advanced technologies such as supercritical fluid extraction, ultra-filtration, and HPLC-MS standardization. For markets like Tonga, establishing robust supply chain transparency, reliable cold-chain or stable powder preservation, and compliance with international pharmacopeia standards are paramount for sustainable health market expansion.
Implementation of AI-monitored extraction parameters ensuring consistent active marker compounds (e.g., Chicoric Acid, Macamides).
Strict adherence to sustainable agricultural harvesting, minimizing environmental footprints across global supply corridors.
Optimized freight and protective packaging designed to withstand tropical marine climates during transit to Tonga.
Our manufacturing facilities operate under strict ISO, GMP, and HACCP compliance frameworks, with multiple organic certifications (USDA/EU) available for specific botanical extracts to meet global import standards.
Yes, we specialize in tailor-made OEM and ODM services, ranging from custom active ingredient concentrations (e.g., standardized polyphenols, chicoric acid) to private-label bulk powder packaging.
All powders are processed in our 100,000-class cleanrooms, vacuum-sealed in multi-layer moisture-proof industrial containers, and rigorously tested via HPLC before dispatch to ensure maximum shelf-life stability.
Explore our comprehensive catalog of 200+ premium botanical extracts designed for global manufacturers and distributors.
 Botanical