Select high-potency standardized plant extracts processed under strict analytical control and targeted for premium life science formulations.
Geneva stands at the intersection of European high-tech development and traditional scientific precision. As a crucial biotech corridor in Western Europe, the city hosts prominent research institutions, global ingredient trading companies, and strict clinical assessment centers. The local industrial infrastructure in Geneva requires botanical raw materials to satisfy the most stringent pharmaceutical and nutraceutical regulations.
By leveraging Geneva's strategic positioning, our manufacturing operations translate raw natural inputs into highly standardized bioactives. This ensures local research laboratories, pharmaceutical developers, and premium cosmetics manufacturers gain immediate access to components featuring superior thermodynamic stability, high solubility, and documented safety profiles.
From a global perspective, the phyto-extraction market is shifting from raw powder formulations toward standardized molecular fractions. Customers no longer just request a plant powder; they specify active biomarkers like *Nobiletin*, *Corosolic Acid*, or *Gingerol* percentages. Our manufacturing protocols align with this development, blending bulk raw materials processing with precise laboratory fractionation.
Every batch produced and distributed through our Geneva hubs complies with European Food Safety Authority (EFSA) criteria, Swiss Quality Standard guidelines, and is accompanied by comprehensive certificates of analysis (COA) verifying clean profiles free from heavy metal residues, pesticides, or organic solvents.
We implement green chemical engineering principles, utilizing water, ethanol, and supercritical CO2 extraction methods to minimize environmental footprints while securing maximum active substance yields.
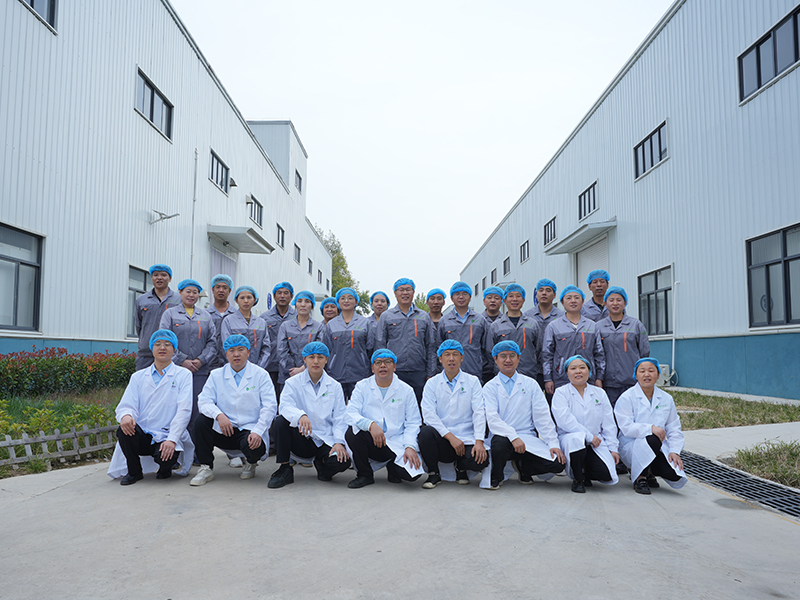
Benefiting from the solid foundation provided by its parent company, Xi'an Tianben Bioengineering Co., Ltd., Botanical Cube Inc. focuses on researching, developing, producing and selling healthy natural ingredients. With more than two decades of industry experience, it has become a leader in the field, specializing in providing high-quality plant extracts and customized solutions to global customers. Services meet the needs of industries including herbal medicine, health foods, dietary supplements, food and beverages, daily chemicals and cosmetics.
Our operations are supported by three companies - Xi'an Tianben Bioengineering Co., Ltd., Botanical Cube Inc. and Shaanxi Tianben Kangyuan Biotechnology Co., Ltd. - which together operate 3 production bases covering more than 100 acres and process more than 3,000 tons of plant raw materials each year. The product range includes more than 200 plant extracts, and we also provide a variety of certified organic products to meet the global demand for environmentally friendly and healthy solutions. Exporting to 60% of the world's countries, serving more than 200 countries and regions and more than 500 customers from all walks of life.
Mapping high-purity natural substances to modern clinical, dietary, and aesthetic solutions in European markets.
Modern European dietary supplements prioritize molecular bioavailability. For instance, combining Piperine with ingredients like Ecdysterone or Berberine HCL enhances absorption rates. Our R&D team provides optimized compound ratios directly to local encapsulation facilities.
Geneva's luxury cosmetics brands require ingredients that are dermatologically safe and clinically proven. Standardized ginger extracts (rich in Gingerols) and loquat leaf extracts are integrated as soothing agents to combat environmental oxidation and aging.
With consumer aversion to synthetic preservatives, natural antioxidants like glucoraphanin from broccoli sprout extract serve dual functions: boosting cellular defenses while acting as natural stabilizers in food matrices.
Our first factory was established in 2012 in Sanyuan City, Xi'an, four years after our company was founded. At that time, our production experience was still in its early stages, and we faced many challenges as we worked to refine our processes. However, we remained committed to continuous improvement, investing heavily in technology, training, and quality control to strengthen our capabilities. These early efforts laid a strong foundation for our future growth, shaping the high standards of excellence that we uphold today.
Powder collection, crushing and sieving, mixing and drying processes are all performed in a Class 100,000 cleanroom environment. Our operators strictly follow hygiene protocols and wear sterile gowns, masks and gloves to maintain product purity and safety, thus ensuring that we provide our customers with high quality standards and reliable ingredients.
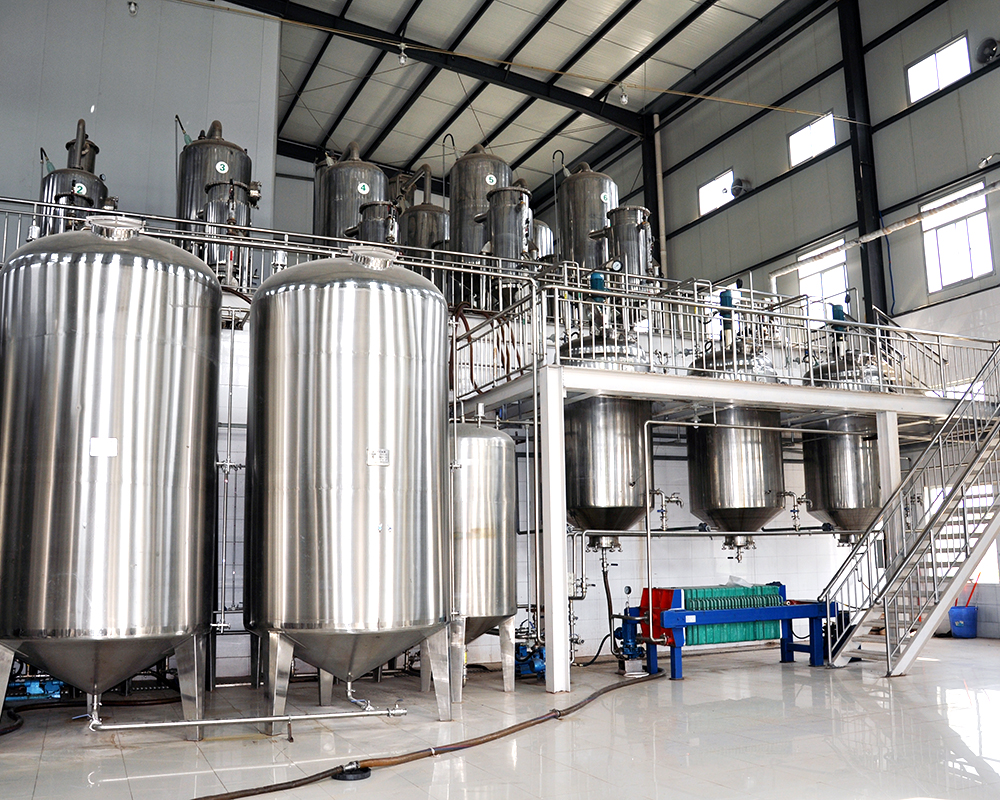
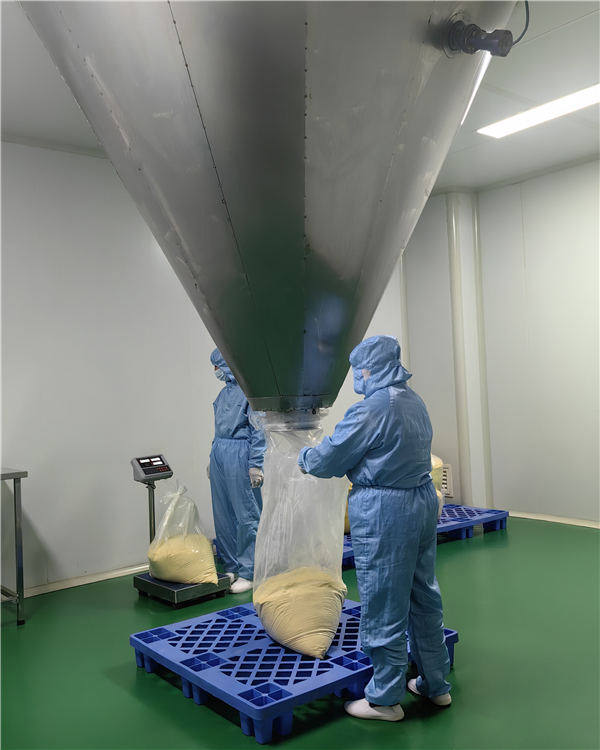
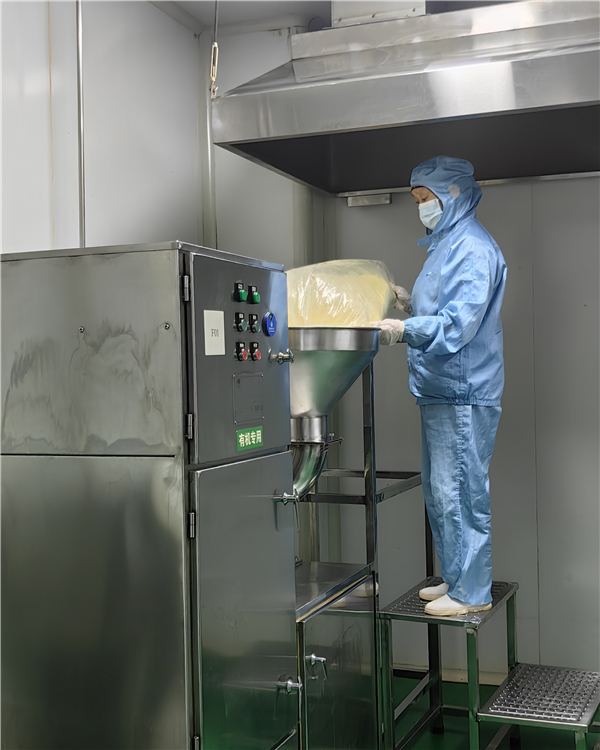
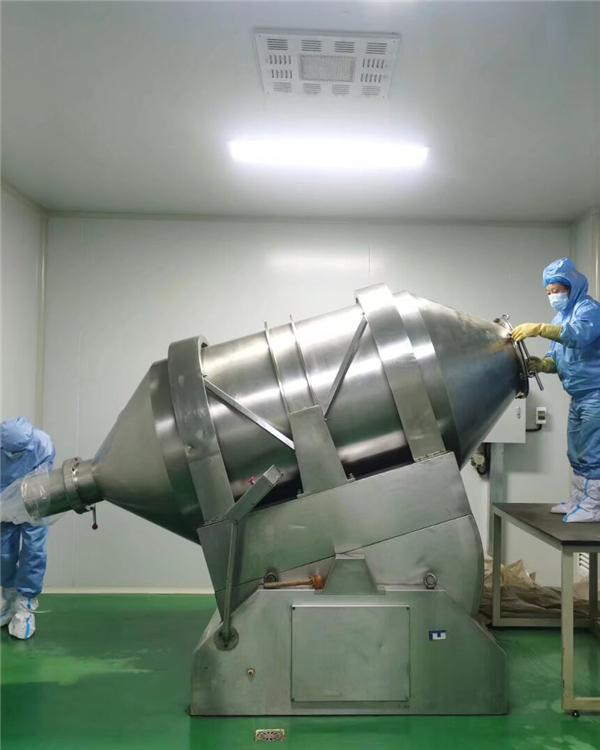
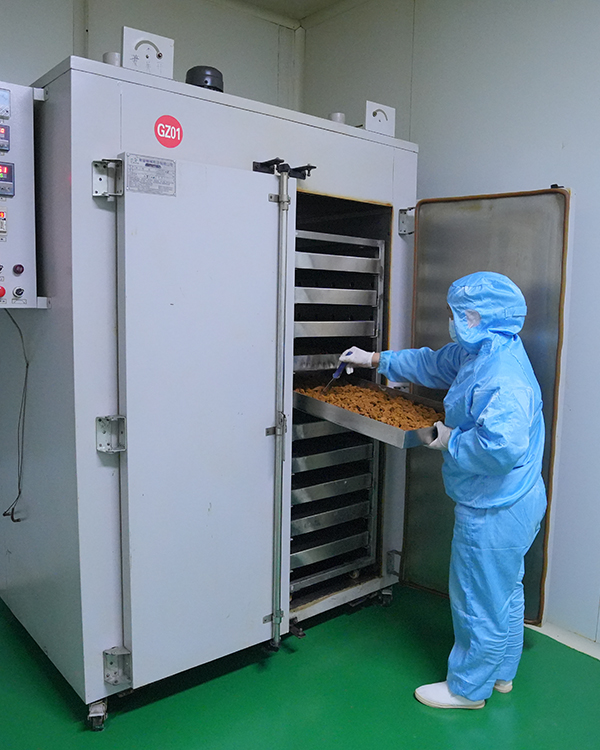
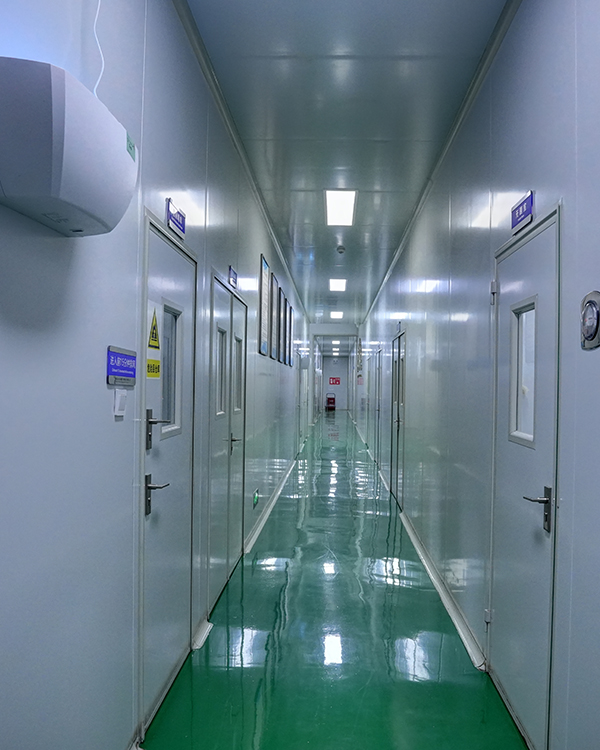
Precision testing and active molecular optimization at every stage of the manufacturing process.
We run Thin-Layer Chromatography (TLC) and High-Performance Liquid Chromatography (HPLC) profiles on all raw botanicals to verify species authenticity, ensuring no cross-contamination occurs before processing.
Our extraction parameters are optimized for each active molecule. For example, utilizing optimized ethanol fractions to target specific gingerol concentrations (5-10%) or isolating pure ecdysterone crystals.
Using low-temperature spray drying and vacuum technologies to maintain the thermal stability of delicate organic fractions, ensuring high solubility and zero degradation.
Addressing technical and logistical questions for global buyers, formulation scientists, and supply chain partners.
Have specific formulation requirements or custom active marker demands?
Contact Our Engineering TeamHigh-purity raw materials designed for food safety, biological activity, and cosmetic stability.
Ensuring precise bio-activity profiles and chemical purity indexes for advanced laboratories.
 Botanical