Engineered high-purity natural extracts optimized for cosmetics, functional foods, and nutraceutical processing within the Rajshahi trade corridor.
Analyzing local shifts toward natural therapeutics and agro-industrial optimization.
The Rajshahi Division, historically known as the agricultural heartland of Bangladesh and celebrated for its thriving silk industry, is currently undergoing a structural economic transformation. Local business leaders and food processors are progressively shifting away from raw crop exports to value-added processing. The demand for organic ingredients is surging as consumer preferences align with wellness, clean label parameters, and chemical-free cosmetics. In particular, sectors like food preservation, dairy processing, specialized wellness formulation, and premium skincare are identifying gaps in their supply chain for high-purity botanicals and biological extracts.
Historically, manufacturers in Rajshahi relied on traditional synthetic preservation techniques or imports from fragmented regional brokers. However, current environmental shifts and strict regulatory compliance enforced by local food standards authorities (BSTI) have heightened the necessity for standardized, bio-active organic additives. The application of biological compounds like Organic Phycocyanin, plant-based polyphenols, and active enzymes has demonstrated the capability to extend shelf-life, enhance cosmetic efficacy, and enrich nutritive indices, providing local processors with a competitive edge in both domestic and regional markets.
Development of targeted dietary supplements utilizing standardized plant extracts for localized health concerns.
Replacing artificial stabilizers with natural mucins and acids to align with modern dermatologist-grade standards.
Transforming Rajshahi's rich agricultural outputs into functional food materials enriched with natural antioxidants.
A Global Leader in Natural Ingredients
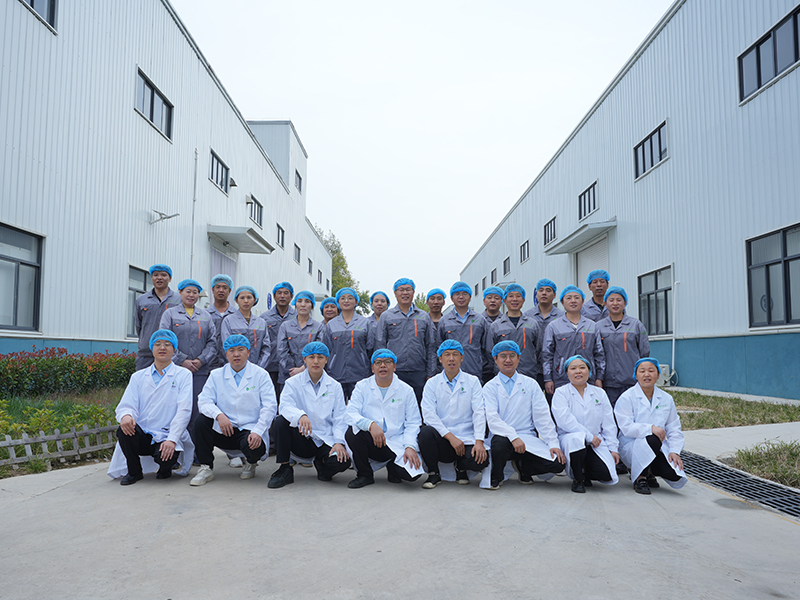
Benefiting from the solid foundation provided by its parent company, Xi'an Tianben Bioengineering Co., Ltd., Botanical Cube Inc. focuses on researching, developing, producing and selling healthy natural ingredients. With more than two decades of industry experience, it has become a leader in the field, specializing in providing high-quality plant extracts and customized solutions to global customers. Services meet the needs of industries including herbal medicine, health foods, dietary supplements, food and beverages, daily chemicals and cosmetics.
Our operations are supported by three companies - Xi'an Tianben Bioengineering Co., Ltd., Botanical Cube Inc. and Shaanxi Tianben Kangyuan Biotechnology Co., Ltd. - which together operate 3 production bases covering more than 100 acres and process more than 3,000 tons of plant raw materials each year. The product range includes more than 200 plant extracts, and we also provide a variety of certified organic products to meet the global demand for environmentally friendly and healthy solutions. Exporting to 60% of the world's countries, serving more than 200 countries and regions and more than 500 customers from all walks of life.
Understanding the international compliance, chromatography benchmarks, and certification architectures.
In the global market, "organic" is not merely a marketing term; it is a rigorous regulatory matrix. Leading quality control organizations such as the USDA National Organic Program (NOP) and European Union organic authorities mandate complete traceability from soil preparation to extraction. In addition, the pharmaceutical-grade extraction industry utilizes precise techniques to isolate individual active phytocompounds (e.g., Luteolin, Phycocyanin, Amla tannins) while maintaining their biochemical integrity. This requires state-of-the-art analytical equipment including High-Performance Liquid Chromatography (HPLC) and Gas Chromatography-Mass Spectrometry (GC-MS) to guarantee active ingredient concentration and verify the absolute absence of heavy metal residuals, pesticide residues, and microbial contamination.
For processors in the Rajshahi region, importing ingredients from a supplier that maintains these global standards eliminates local testing bottlenecks. When active ingredients are certified by international frameworks (such as ISO 22000, GMP, Kosher, and Halal), the resulting localized products are immediately positioned for export to Western markets. This global compliance architecture creates a seamless path for local manufacturers to scale their brands internationally, backed by third-party certified batch records and certificates of analysis (COAs).
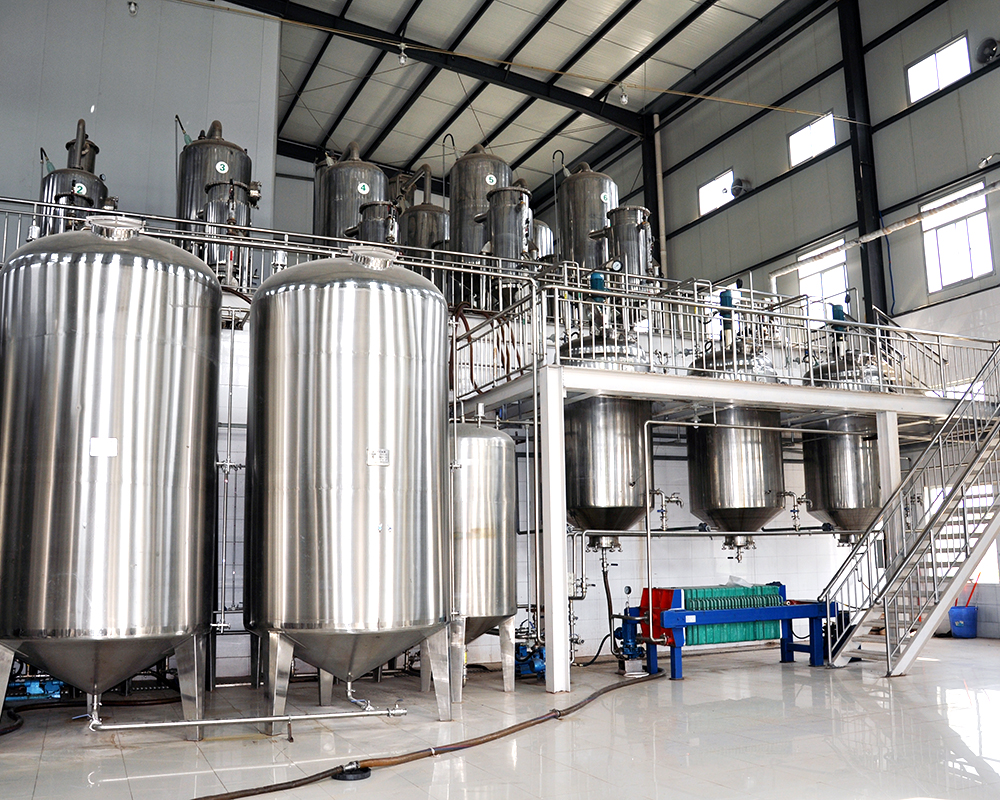
Our first factory was established in 2012 in Sanyuan City, Xi'an, four years after our company was founded. At that time, our production experience was still in its early stages, and we faced many challenges as we worked to refine our processes. However, we remained committed to continuous improvement, investing heavily in technology, training, and quality control to strengthen our capabilities. These early efforts laid a strong foundation for our future growth, shaping the high standards of excellence that we uphold today.
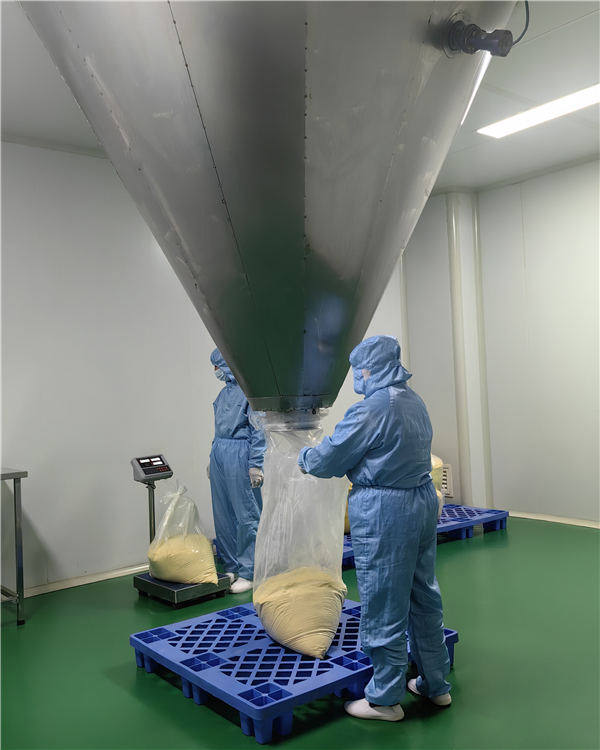
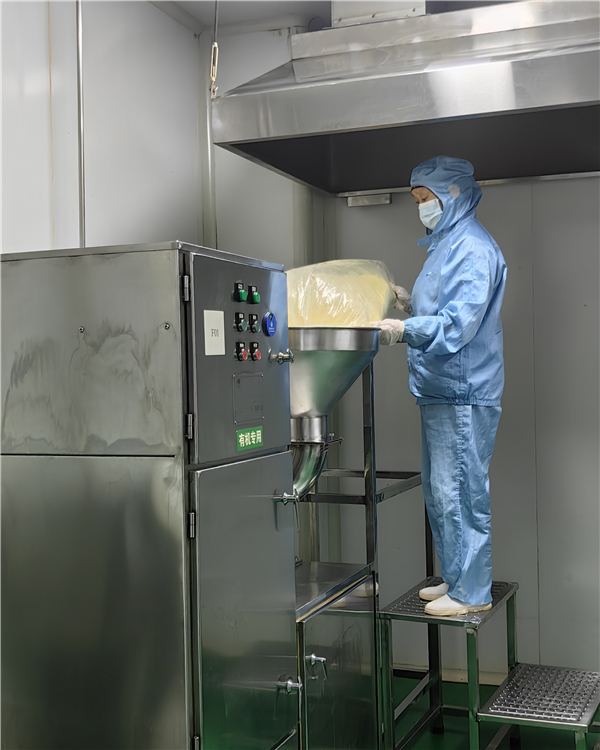
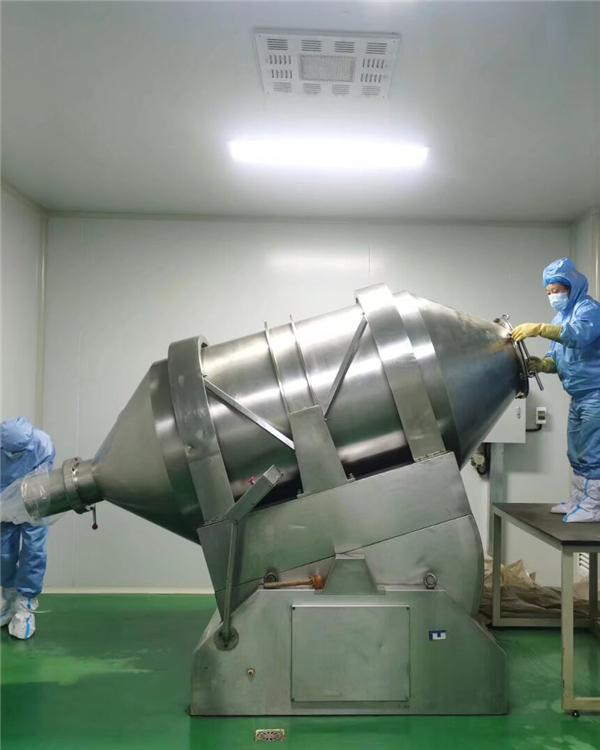
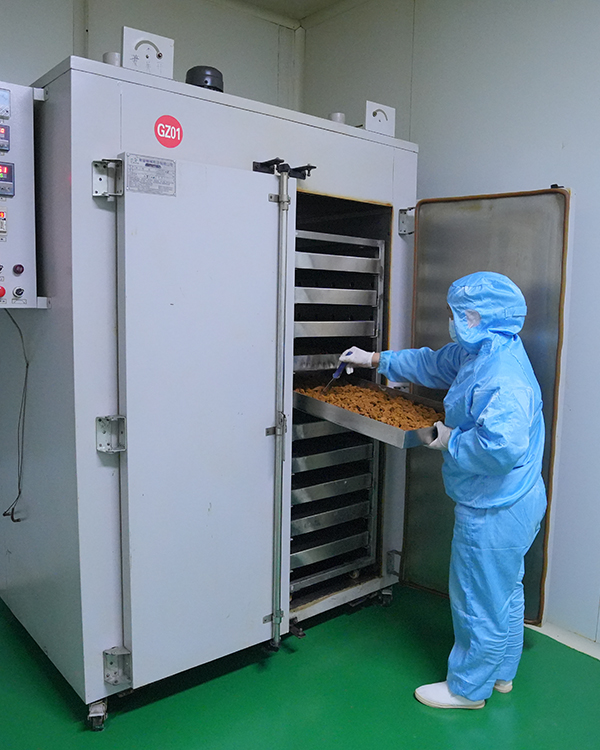
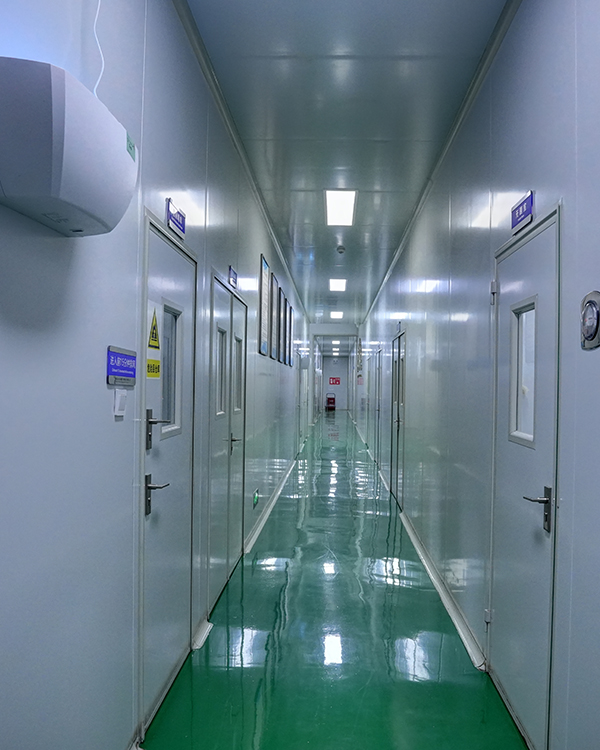
Powder collection, crushing and sieving, mixing and drying processes are all performed in a Class 100,000 cleanroom environment. Our operators strictly follow hygiene protocols and wear sterile gowns, masks and gloves to maintain product purity and safety, thus ensuring that we provide our customers with high quality standards and reliable ingredients.
Why specialized manufacturing clusters in China represent the most reliable procurement channel for South Asian markets.
The global bio-active ingredient sector relies heavily on Chinese extraction clusters for several core reasons: scale, raw material vertical integration, and continuous manufacturing technology. Factories in Shaanxi province, such as our parent company's ecosystem, benefit from proximity to vast geographical growing regions (e.g., Qinling Mountains for wild botanicals, North-Western farming zones for grains and seeds). By controlling raw crop sourcing and running automated continuous counter-current extraction systems, Chinese factories achieve economies of scale that are impossible to duplicate in localized regional extraction setups. Processing thousands of metric tons per year ensures that chemical reagents, energy consumption, and high-performance labor are optimized, driving down unit costs while maintaining superior purity indexes.
For import-reliant regions like Rajshahi, purchasing directly from a Chinese factory ecosystem eliminates the multiple markup layers added by trading houses and regional middlemen. Furthermore, our dedicated container logistics, standard packaging (double food-grade PE bags inside fiber drums), and customs clearance expertise minimize lead times. This direct integration guarantees supply chain resilience, protecting local companies in Bangladesh from seasonal pricing spikes and product shortages.
Custom solutions addressing specific local industries, climatic challenges, and manufacturing trends.
Rajshahi is globally famous for its premium mangoes and agricultural yields. Utilizing natural antioxidants such as Mangosteen Extract and Amla Extract allows regional processors to formulate organic preservation coatings and active functional juices, inhibiting enzymatic browning and maintaining nutrient levels naturally.
With high temperatures and humidity characterizing Rajshahi's climate, local skincare developers require stable, non-greasy ingredients. Formulating with high-purity Hyaluronic Acid and Snail Mucin Powder enables the production of quick-absorbing serums that replenish moisture levels without blocking pores.
As lifestyle-related health awareness grows across major urban centers in Bangladesh, the integration of premium botanical actives like Luteolin (for neuroprotection) and Bifidobacterium (for gut microbiome balance) into dry beverages and daily supplements is gaining significant market traction.
Deciphering the evolution of plant extraction technologies and biological active delivery systems over the next decade.
The global organic active marketplace is undergoing a profound paradigm shift: moving away from crude herbal powders toward specialized, standardized, and bioavailable active matrices. Over the next decade, technology will focus on enhancing cell absorption. Standard botanical extracts often suffer from low bio-absorption rates when passing through the human digestive tract. To solve this problem, advanced encapsulation technologies like Liposomal encapsulation (as seen in our Liposomal Vitamin C) are becoming the industry gold standard. These lipid spheres shield fragile active nutrients from stomach acid degradation, delivering them directly into the bloodstream.
Simultaneously, the demand for natural alternatives to synthetic food colorants is growing exponentially. Natural blues and greens, traditionally difficult to stabilize, are now effectively formulated using stable Phycocyanin and Butterfly Pea extracts. These botanical sources provide rich color pigments while offering secondary therapeutic benefits, such as antioxidant properties. Manufacturers in Rajshahi who adopt these advanced ingredients today are positioning themselves ahead of the curve, preparing for a future where consumers will reject synthetic additives entirely.
Standardized natural powders engineered to support high-performance formulations.
Reviewing extraction precision and scientific criteria required to establish ingredient reliability.
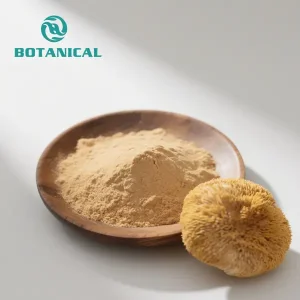
For buyers in Rajshahi's competitive manufacturing sector, the primary challenge is verifying that raw material certificates match reality. The phytochemical verification process is critical. A high-quality extraction facility utilizes precise scientific protocols to ensure chemical consistency. For instance, Luteolin and Hericium Erinaceus (Lion's Mane) extract must undergo rigorous fingerprinting. Liquid chromatography shows the presence of specialized polysaccharides and flavones. Without these testing systems, buyers are vulnerable to purchasing adulterated products.
Additionally, microbial stability is critical when shipping raw botanical powders to warm regions like Rajshahi. The humidity during marine shipping from China through Chittagong Port can degrade active ingredients if packaging standards are sub-par. Our factory solves this by applying strict vacuum sealing and double-layered heat-sealed aluminum pouches, packed inside dry, high-density fiber drums. We also test each batch for yeast, mold, and bacterial pathogens like E. coli and Salmonella inside our Class 100,000 cleanroom, ensuring that the raw material arrives at your facility ready for immediate production.
Direct factory efficiency scaling biological manufacturing on a global level.
High-purity phytochemicals, standardized vitamins, and probiotic ingredients serving the Rajshahi industrial region.
Essential purchasing protocols, pricing structures, and maritime trade management from China to Bangladesh.
Procuring raw materials from Chinese manufacturing hubs requires an understanding of standard B2B import procedures. When purchasing active ingredients like Organic Blue Spirulina or Hyaluronic Acid, buyers in Rajshahi should establish several parameters with their logistics partners:
By establishing these checkpoints, Rajshahi-based manufacturers can guarantee product consistency, prevent port-of-entry delays, and maintain lean manufacturing inventory schedules.
Addressing technical, logistical, and commercial inquiries for manufacturers in Rajshahi and the global market.
Get in touch with our technical sales division to request custom quotations, raw material samples, or technical specification dossiers tailored to the Rajshahi industrial market.
 Botanical