Explore our core bio-active extracts manufactured under strict cGMP protocols for high efficacy custom blends.
The shift from single-ingredient extracts to multi-pathway bio-available antioxidant complexes in the global wellness market.
The global functional food, beverage, and dietary supplement markets are undergoing a fundamental paradigm shift. Historically, product formulators relied on isolated single-ingredient botanical powders, such as basic acai or wild blueberry powders. However, modern scientific literature and consumer awareness have exposed the limitations of single-molecule supplements. Today, commercial buyers seek synergistic Superfruit Extract Mixes engineered to deliver comprehensive cellular protection, enhanced bioavailability, and targeted metabolic outcomes.
According to current market intelligence, the global market for superfruit extracts is projected to expand at a compound annual growth rate (CAGR) of over 8.4% through 2030. This growth is propelled by rapid innovation in extraction dynamics, low-temperature microencapsulation, and non-destructive drying technologies that preserve delicate phytochemical matrices including polyphenols, anthocyanins, proanthocyanidins, and naturally occurring vitamin derivatives.
How Botanical Cube Inc. applies chemical engineering and strict quality control to guarantee active molecule activity.
Superfruit formulations require advanced extraction and preservation methodologies to ensure that key thermolabile compounds—such as anthocyanidins, vitamin C, rosmarinic acid, and carnosic acid—do not undergo oxidative degradation during manufacturing. Our operations leverage Low-Temperature Vacuum Microwave Extraction (LTVME) and Supercritical CO₂ Fluid Extraction to achieve hyper-purified extract yields without solvent residue contamination.
| Botanical Ingredient Mix Component | Standardized Active Marker | Testing Methodology | Functional Efficacy Focus |
|---|---|---|---|
| Organic Acerola & Berry Complex | 25% Natural Vitamin C, 15% Polyphenols | HPLC / UV-Vis | Cellular Antioxidant & Immune Support |
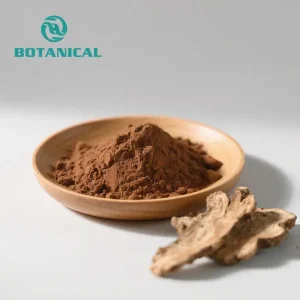
| Ashwagandha & Adaptogen Matrix | 5% - 10% Withanolides | HPLC Internal Standard | Cortisol Regulation & Stress Adaptation |
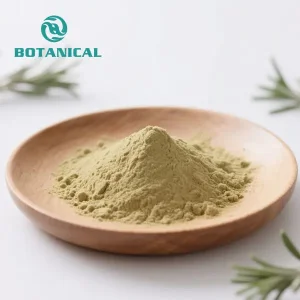
| Rosmarinus Officinalis Extract | 20% Carnosic Acid, 15% Rosmarinic Acid | HPLC-MS/MS | Lipid Oxidation Resistance & Shelf Stabilization |
| Chaga & Functional Mushroom Matrix | 30% Polysaccharides, 10% Beta-Glucans | Enzymatic / Gravimetric Assay | Immune System Modulation & Gut Health |
| Apple Pectin & Botanical Fiber | 65% Soluble Dietary Fiber | AOAC 991.43 Method | Microbiome Support & Formulation Binding |
Backing worldwide supplement brands with reliable continuous supply and massive processing capabilities.
Every batch undergoes high-performance liquid chromatography (HPLC), gas chromatography-mass spectrometry (GC-MS), and heavy metal spectroscopy before dispatch.
Available in 80 to 200 mesh particle sizes, micro-encapsulated for 100% instant cold-water solubility for functional beverage mixes.
Non-GMO, irradiated-free, allergen-free powders fully compatible with USDA Organic, EU Organic, Kosher, and Halal specifications.
A Global Leader in Natural Botanical Ingredients with over two decades of technical expertise.
Benefiting from the solid foundation provided by its parent company, Xi'an Tianben Bioengineering Co., Ltd., Botanical Cube Inc. focuses on researching, developing, producing and selling healthy natural ingredients. With more than two decades of industry experience, it has become a leader in the field, specializing in providing high-quality plant extracts and customized solutions to global customers. Services meet the needs of industries including herbal medicine, health foods, dietary supplements, food and beverages, daily chemicals and cosmetics.
Our operations are supported by three companies—Xi'an Tianben Bioengineering Co., Ltd., Botanical Cube Inc. and Shaanxi Tianben Kangyuan Biotechnology Co., Ltd.—which together operate 3 production bases covering more than 100 acres and process more than 3,000 tons of plant raw materials each year. The product range includes more than 200 plant extracts, and we also provide a variety of certified organic products to meet the global demand for environmentally friendly and healthy solutions. Exporting to 60% of the world's countries, serving more than 200 countries and regions and more than 500 customers from all walks of life.
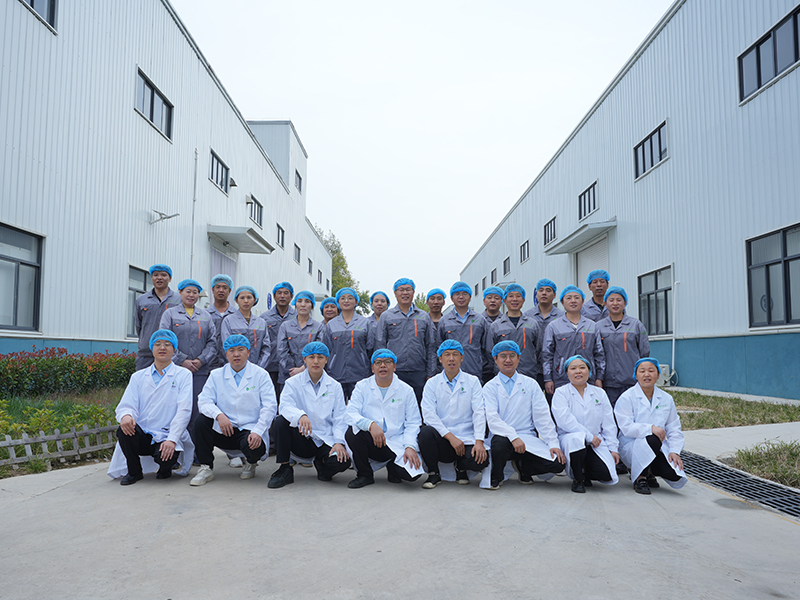
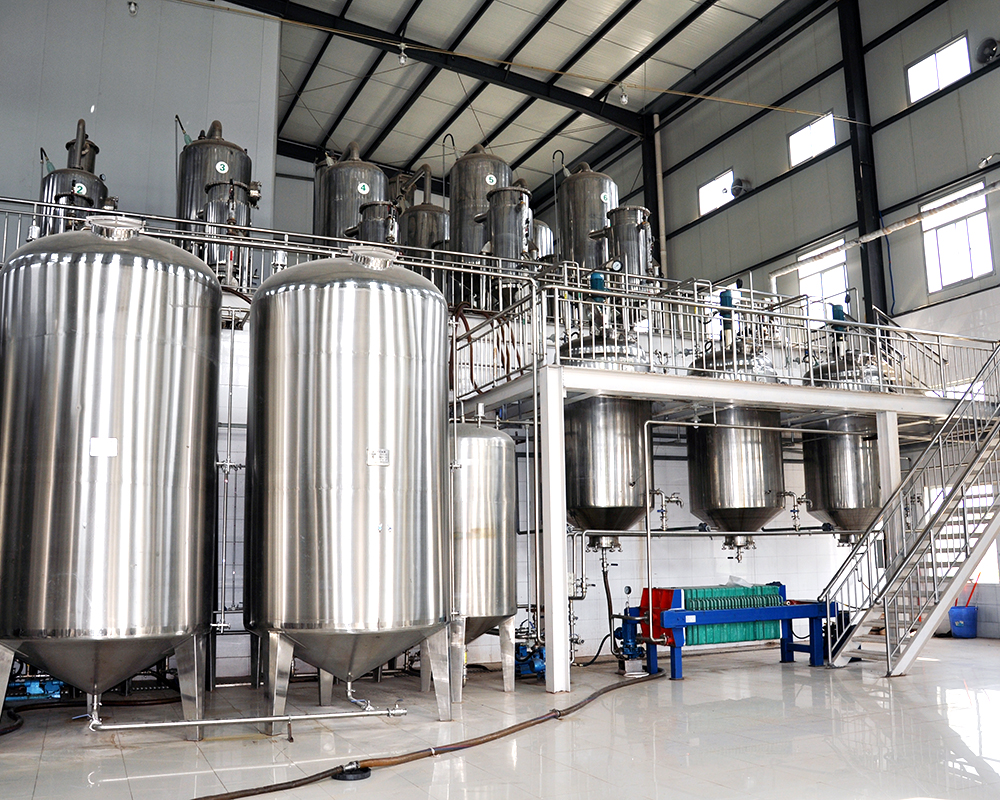
Our first factory was established in 2012 in Sanyuan City, Xi'an, four years after our company was founded. At that time, our production experience was still in its early stages, and we faced many challenges as we worked to refine our processes. However, we remained committed to continuous improvement, investing heavily in technology, training, and quality control to strengthen our capabilities. These early efforts laid a strong foundation for our future growth, shaping the high standards of excellence that we uphold today.
Powder collection, crushing and sieving, mixing and drying processes are all performed in a Class 100,000 cleanroom environment. Our operators strictly follow hygiene protocols and wear sterile gowns, masks and gloves to maintain product purity and safety, thus ensuring that we provide our customers with high quality standards and reliable ingredients.
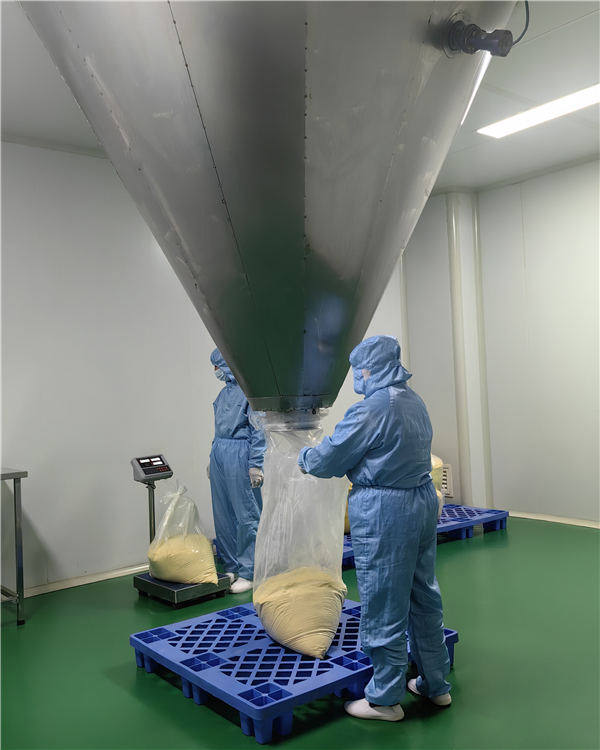
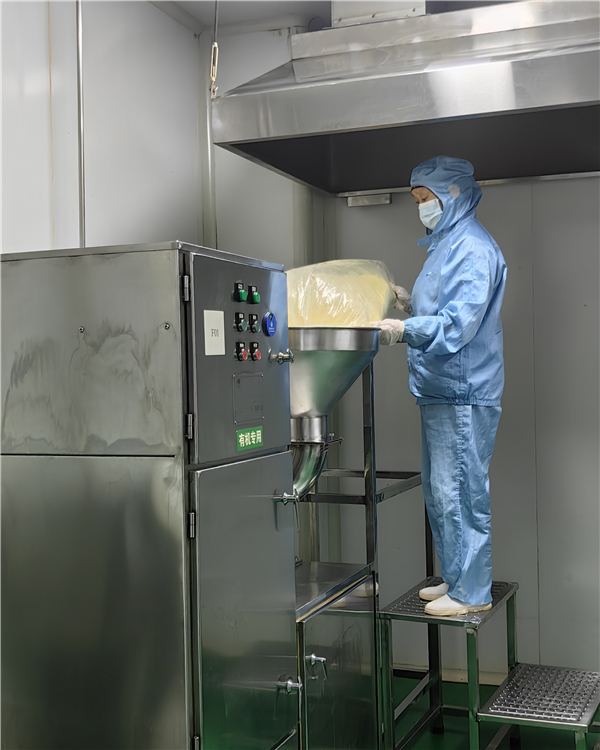
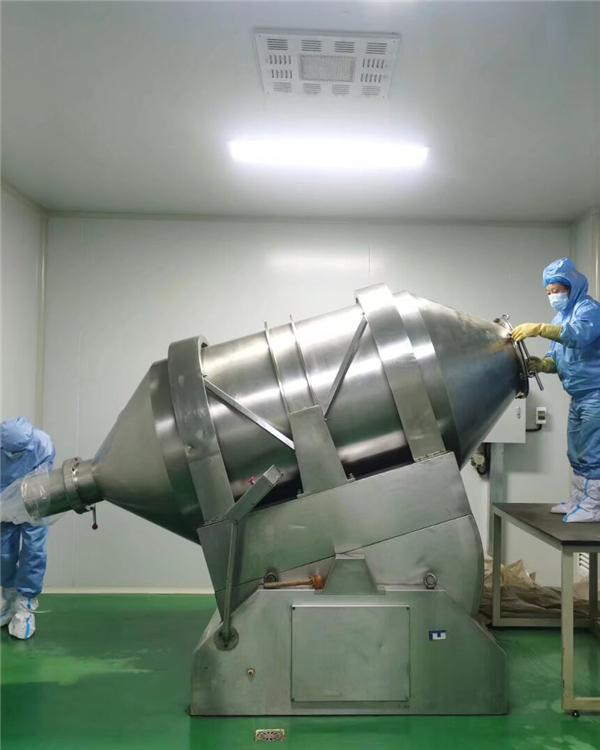
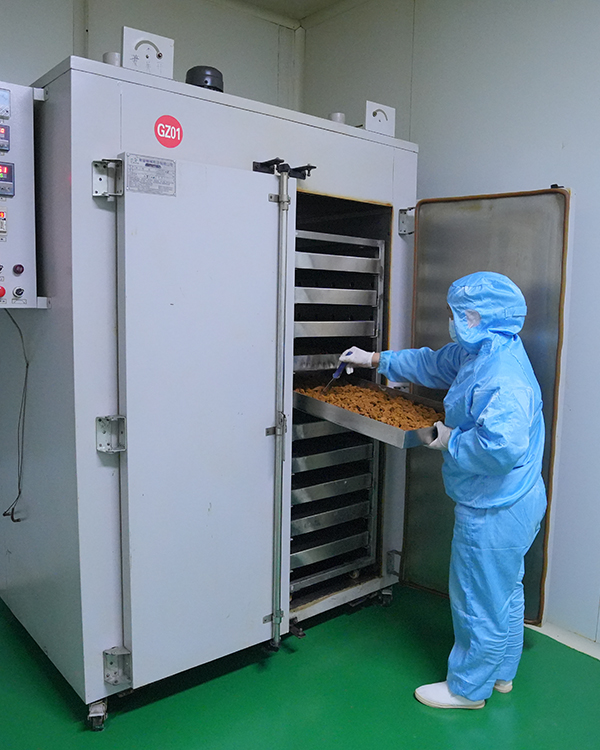
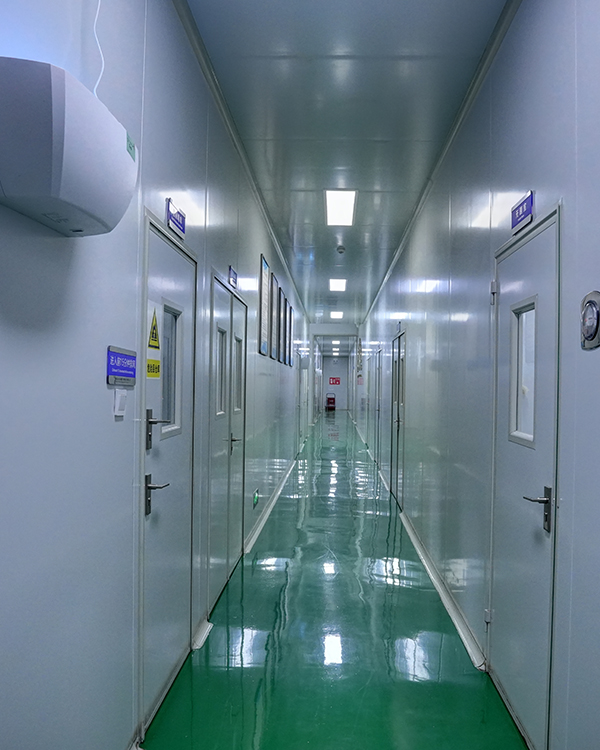
Overcoming compliance hurdles, regional ingredient quotas, and custom dosage formulation challenges.
Pioneering green biotechnology for enhanced stability and targeted bio-accessibility.
Looking toward 2030, Botanical Cube Inc. is actively scaling two major R&D breakthroughs for our wholesale partners:
By treating high-molecular weight polyphenols with natural glycosidases, we break down large sugar moieties into aglycone forms. This process drastically improves intestinal absorption speeds, allowing consumers to experience maximum antioxidant bio-availability at lower milligram dosages.
Combining spray drying with cryogenic freezing preserves thermolabile phytonutrients and anthocyanins that traditional spray drying degrades. Phospholipid liposomal encapsulation shields active ingredients from stomach acids for targeted release in the small intestine.
Expand your product pipeline with certified pure botanical powders and specialized ingredients.
Technical and logistical answers for wholesale buyers, product managers, and formulation engineers.
 Botanical