Explore our high-demand OEM/ODM natural extracts and functional ingredients tailored for global markets.
A Global Leader in Natural Ingredients & Advanced Botanical Processing
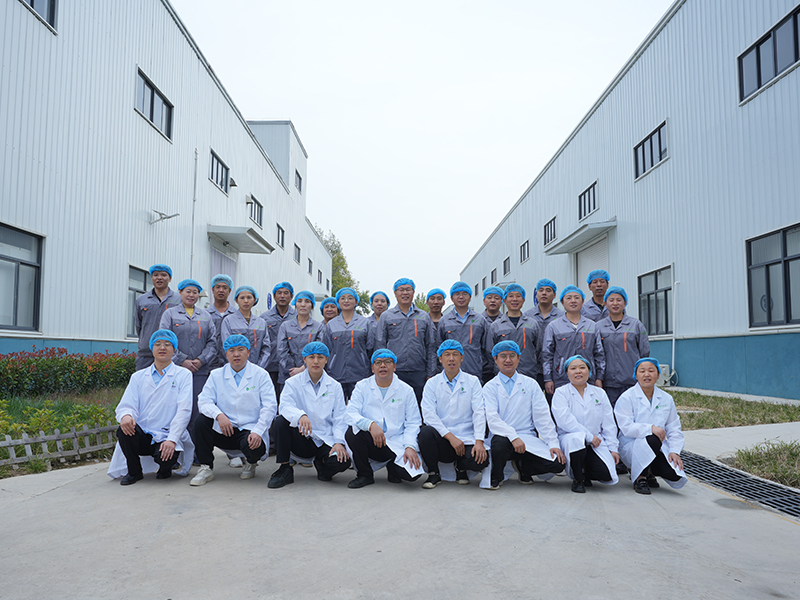
Benefiting from the solid foundation provided by its parent company, Xi'an Tianben Bioengineering Co., Ltd., Botanical Cube Inc. focuses on researching, developing, producing and selling healthy natural ingredients. With more than two decades of industry experience, it has become a leader in the field, specializing in providing high-quality plant extracts and customized solutions to global customers. Services meet the needs of industries including herbal medicine, health foods, dietary supplements, food and beverages, daily chemicals and cosmetics.
Our operations are supported by three companies - Xi'an Tianben Bioengineering Co., Ltd., Botanical Cube Inc. and Shaanxi Tianben Kangyuan Biotechnology Co., Ltd. - which together operate 3 production bases covering more than 100 acres and process more than 3,000 tons of plant raw materials each year. The product range includes more than 200 plant extracts, and we also provide a variety of certified organic products to meet the global demand for environmentally friendly and healthy solutions. Exporting to 60% of the world's countries, serving more than 200 countries and regions and more than 500 customers from all walks of life.
Rigorous Standards of Purity and Production Mastery
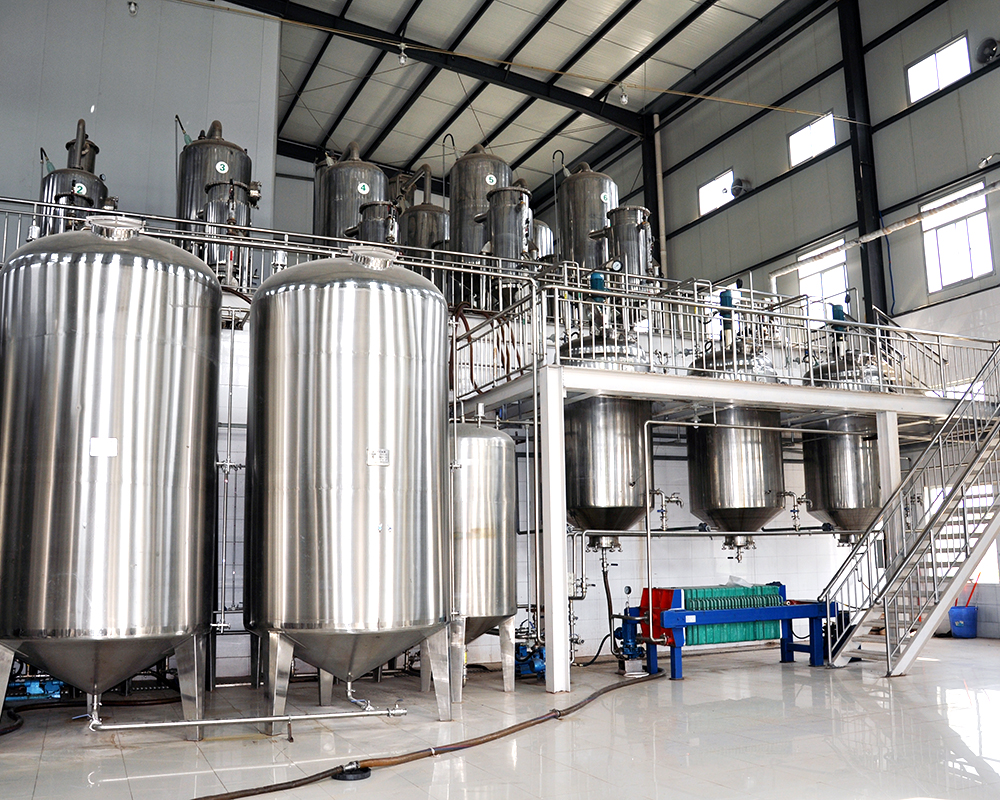
Our first factory was established in 2012 in Sanyuan City, Xi'an, four years after our company was founded. At that time, our production experience was still in its early stages, and we faced many challenges as we worked to refine our processes. However, we remained committed to continuous improvement, investing heavily in technology, training, and quality control to strengthen our capabilities. These early efforts laid a strong foundation for our future growth, shaping the high standards of excellence that we uphold today.
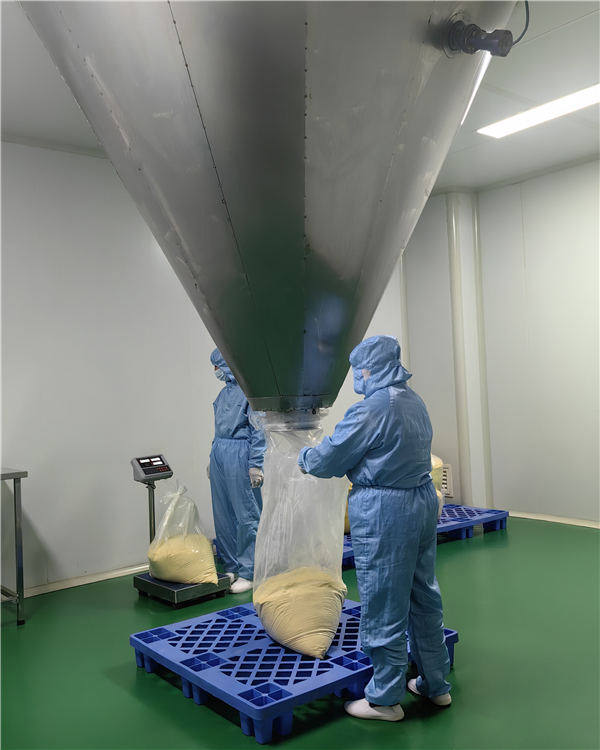
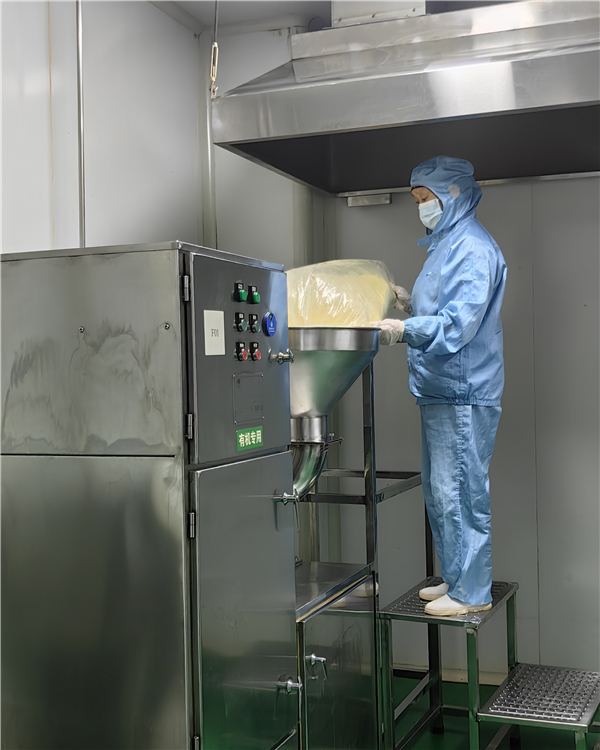
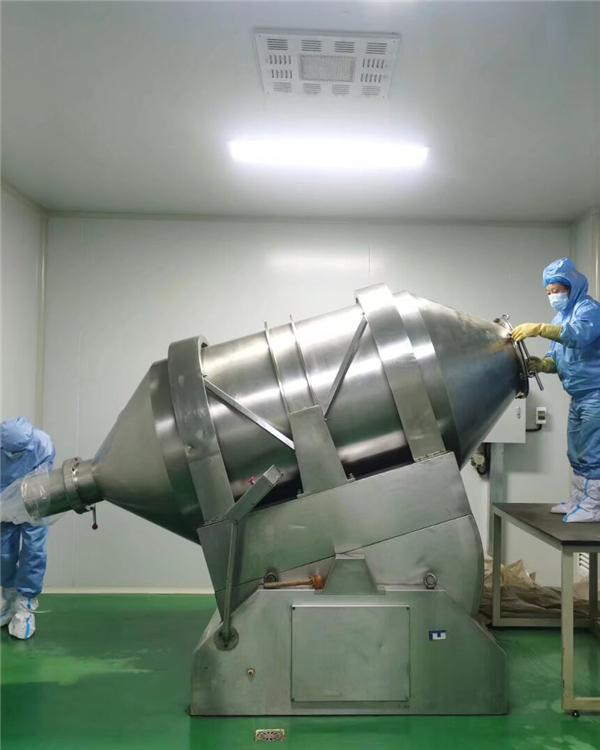
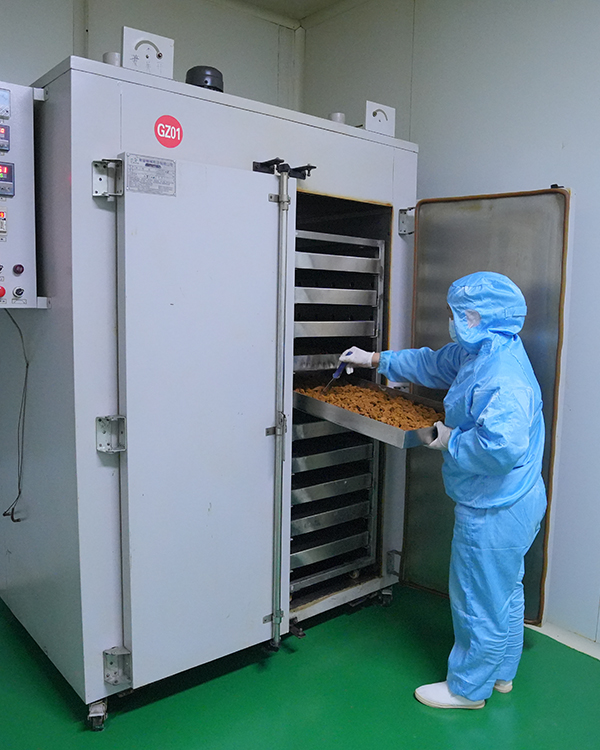
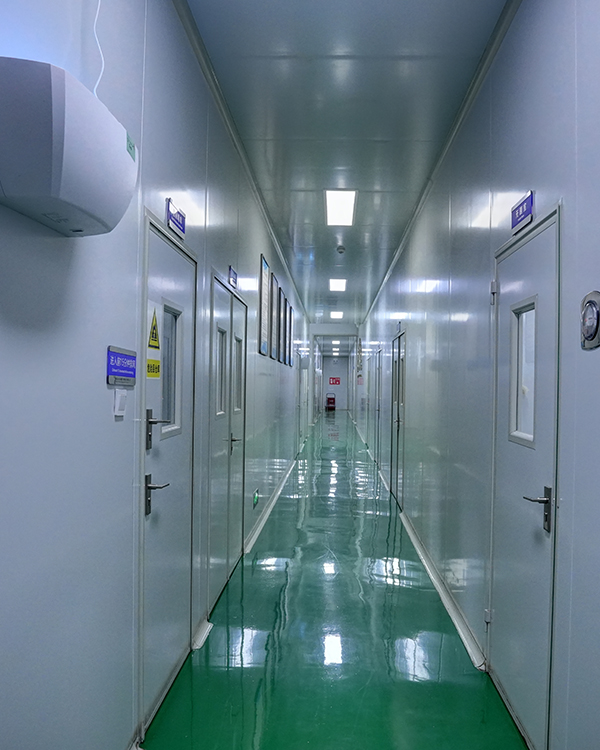
Powder collection, crushing and sieving, mixing and drying processes are all performed in a Class 100,000 cleanroom environment. Our operators strictly follow hygiene protocols and wear sterile gowns, masks and gloves to maintain product purity and safety, thus ensuring that we provide our customers with high quality standards and reliable ingredients.
Empowering Global Enterprises with End-to-End OEM/ODM Solutions
Tons of raw plant materials processed annually, guaranteeing consistent bulk supply and competitive pricing advantages.
Standardized plant extracts and custom formulations designed to match regional regulatory requirements across 60+ countries.
Global brand partners relying on our localized R&D support, agile logistics, and strict compliance assurance.
Meeting Rigorous Industry Demands Through Tailored Formulation Engineering
Modern nutraceutical, cosmetic, and functional food brands face intense competition and stringent regulatory frameworks (such as FDA, EFSA, and USP standards). Partnering with a premier OEM ODM extract manufacturer like Botanical Cube Inc. provides immediate risk mitigation. We ensure raw material traceability, verified marker compound assays (via HPLC/GC-MS), and robust documentation support that accelerates market entry for our international clients.
Our botanical extracts and active ingredients seamlessly integrate into diverse downstream markets:
Driving Innovation Through Sustainable Sourcing & Green Chemistry
Consumers globally prioritize transparency, demanding non-GMO, organic, and clean-label certifications. Our agricultural partnerships ensure certified organic sourcing from cultivation to finished powder.
Moving beyond traditional solvent methods, supercritical fluid extraction and ultrasonic-assisted processing maximize active ingredient yield while minimizing environmental footprints.
Brand differentiation relies on proprietary blends. Our R&D team collaborates closely with clients to formulate customized synergistic botanical complexes tailored to specific health outcomes.
Expert Insights into Our OEM/ODM Manufacturing and Supply Capabilities
A: As a direct manufacturer with large-scale production bases processing over 3,000 tons of raw materials annually, we offer flexible MOQ terms depending on whether the product is a standard stock extract or a specialized custom formulation. Contact our sales engineering team for detailed project specifications.
A: All production stages—including powder collection, crushing, sieving, mixing, and drying—are conducted inside our 100,000-class cleanroom environment. Every batch undergoes rigorous testing for heavy metals, microbial limits, and active marker assays, backed by full COA, MSDS, and third-party lab verification.
A: Yes. We specialize in OEM and ODM services, ranging from custom ingredient blending and standardized active assay adjustments to bespoke packaging and private labeling designed to meet your brand's regional market requirements.
A: We export to over 60 countries and regions worldwide, serving more than 500 enterprise clients across the dietary supplement, functional food and beverage, cosmetics, and herbal pharmaceutical industries.
Discover more specialized wholesale solutions from our extensive manufacturing catalog.
 Botanical