Explore our premium grade active botanical ingredients engineered for superior potency and purity.
Benefiting from the solid foundation provided by its parent company, Xi'an Tianben Bioengineering Co., Ltd., Botanical Cube Inc. focuses on researching, developing, producing and selling healthy natural ingredients. With more than two decades of industry experience, it has become a leader in the field, specializing in providing high-quality plant extracts and customized solutions to global customers. Services meet the needs of industries including herbal medicine, health foods, dietary supplements, food and beverages, daily chemicals and cosmetics.
Our operations are supported by three companies - Xi'an Tianben Bioengineering Co., Ltd., Botanical Cube Inc. and Shaanxi Tianben Kangyuan Biotechnology Co., Ltd. - which together operate 3 production bases covering more than 100 acres and process more than 3,000 tons of plant raw materials each year. The product range includes more than 200 plant extracts, and we also provide a variety of certified organic products to meet the global demand for environmentally friendly and healthy solutions. Exporting to 60% of the world's countries, serving more than 200 countries and regions and more than 500 customers from all walks of life.
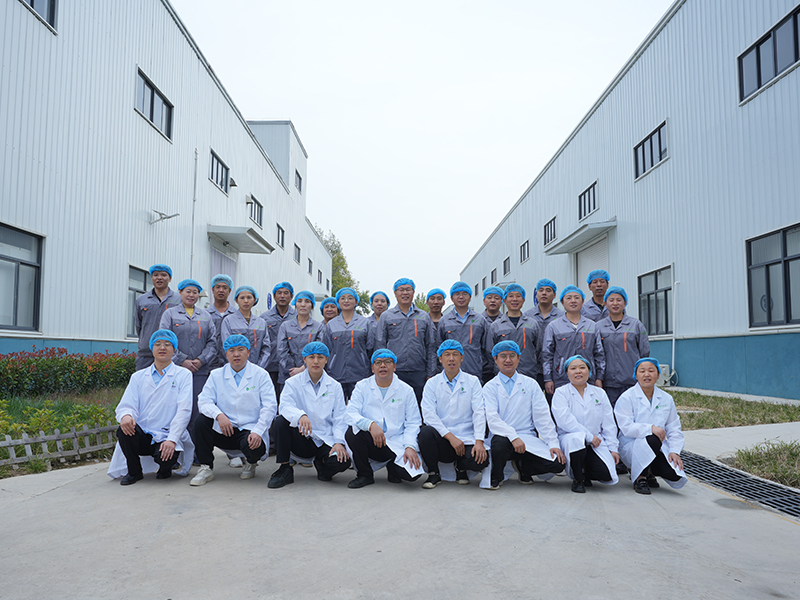
Advanced manufacturing standards ensuring absolute purity and safety.
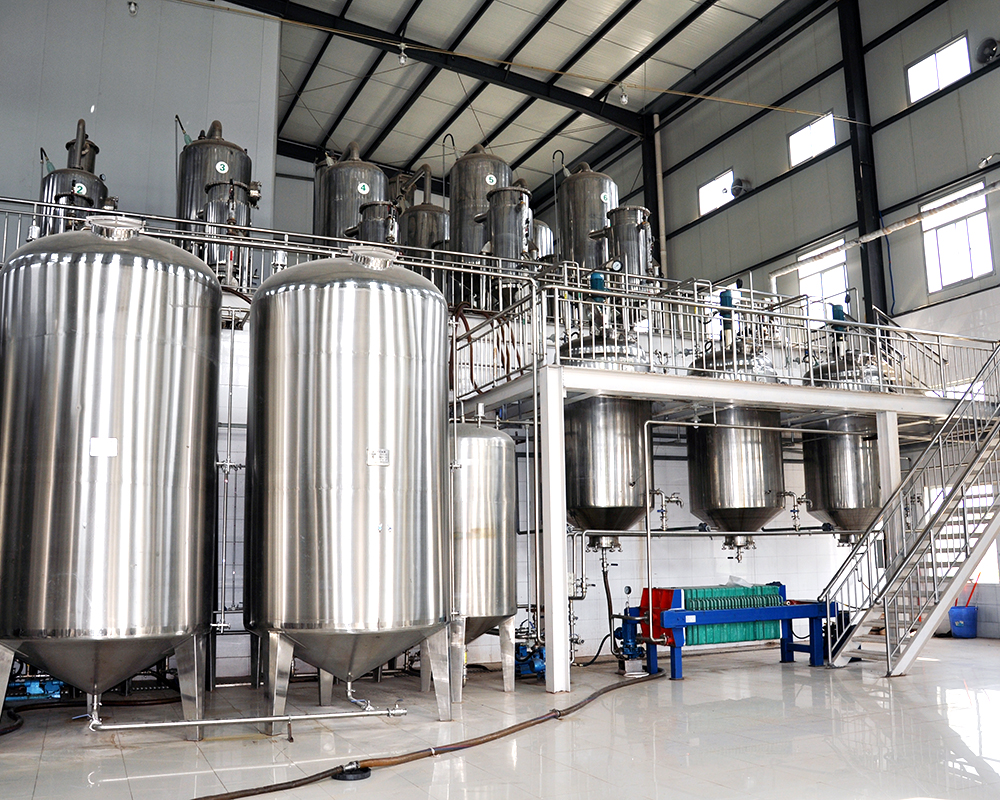
Our first factory was established in 2012 in Sanyuan City, Xi'an, four years after our company was founded. At that time, our production experience was still in its early stages, and we faced many challenges as we worked to refine our processes. However, we remained committed to continuous improvement, investing heavily in technology, training, and quality control to strengthen our capabilities. These early efforts laid a strong foundation for our future growth, shaping the high standards of excellence that we uphold today.
Powder collection, crushing and sieving, mixing and drying processes are all performed in a Class 100,000 cleanroom environment. Our operators strictly follow hygiene protocols and wear sterile gowns, masks and gloves to maintain product purity and safety, thus ensuring that we provide our customers with high quality standards and reliable ingredients.
Providing deep information gain through empirical data and specialized industrial insights.
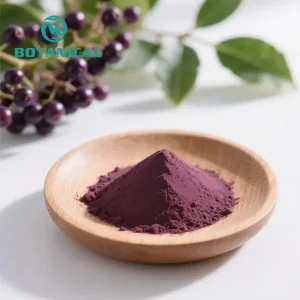
Utilizing state-of-the-art supercritical CO2 extraction and low-temperature membrane concentration technologies, our mixed berry extracts preserve fragile anthocyanins, ellagitannins, and pterostilbenes without thermal degradation.
Our ongoing R&D roadmap incorporates AI-driven chromatographic fingerprinting, ensuring batch-to-batch standardization and maximum bioavailability for nutraceutical formulators worldwide.
Mixed berry extracts are rapidly expanding across functional beverages, dietary supplements, and cosmeceuticals. In North American and European markets, consumers prioritize immune support, anti-aging, and cognitive enhancement.
Localized applications include customized functional gummies, effervescent tablets, and advanced antioxidant serums tailored to specific regional regulatory frameworks and clean-label preferences.
Our integrated supply chain model across Shaanxi Province mitigates global logistics disruptions through strategic raw material sourcing, robust inventory buffering, and highly automated processing lines.
This operational excellence guarantees uninterrupted supply stability, cost-efficiency, and strict adherence to international quality standards such as ISO, cGMP, HACCP, and USDA Organic.
Expert answers regarding our manufacturing capabilities and technical specifications.
Our standard mixed berry extract formulations are typically standardized to 25% total anthocyanins via HPLC testing, though custom concentrations ranging from 10% to 50% are fully supported for OEM/ODM clients.
We source directly from certified sustainable agricultural cooperatives across prime growing regions. Each batch undergoes rigorous heavy metal, pesticide residue, and microbial testing in our ISO-accredited laboratory.
To support growing brands and enterprise partners alike, our standard MOQ starts at 25kg for stock botanical powders, while customized phytonutrient blends can be scaled according to specific project requirements.
Yes, we supply comprehensive documentation including Certificates of Analysis (CoA), Material Safety Data Sheets (MSDS), non-GMO statements, allergen declarations, and organic certificates for smooth customs clearance worldwide.
Discover additional high-purity botanical extracts and functional ingredient solutions.
 Botanical